
Equipment
Vertical Mixer Machine
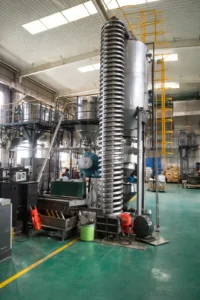
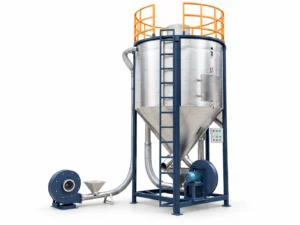
Vertical screw batch mixer for large-capacity blending, batch homogenization, and color mixing of plastic pellets, regrind flakes, and granular masterbatches.
Equipment Selection
CPEA Approved Article (China Plastics Equipment Alliance)
How controlled mixing reduces batch variation in plastic recycling and compounding: vertical silo mixers for bulk PP and HDPE pellets, ribbon blenders for powders and sensitive granules.
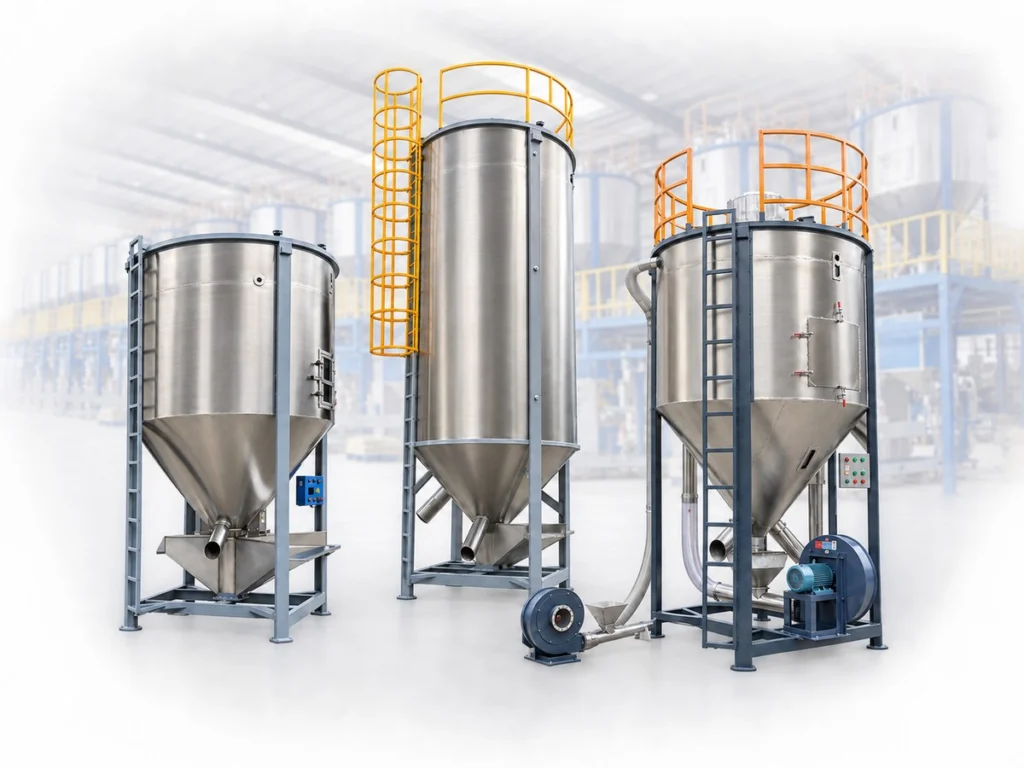
I have seen how expensive unstable material becomes. When every batch behaves differently, the production team spends its time adjusting the line and investigating defects.
Mixers reduce differences within and between plastic material batches and distribute measured ingredients before processing. In recycling and compounding pelletizing, controlled blending produces more consistent feedstock. I select vertical silo mixers for suitable pellets and rigid flakes, and horizontal ribbon blenders for suitable powders and more demanding formulations.
I approach selection from a factory owner’s position: predictable production, manageable operating costs, and material that meets the agreed specification.
At Nicety Machinery Co., Ltd. we build auxiliary equipment and integrated systems for plastic modification, pelletizing and engineering plastics processing, and we treat material mixing as part of that complete production process.
Before choosing a machine, I ask three questions: what variation am I trying to control, what form does the material take, and how will it reach the next process without losing its uniformity?
Those questions matter more than the largest tank or the lowest purchase price.
I cannot expect steady production when the material entering the extruder changes throughout the shift. Repeated machine adjustments can hide the underlying material problem.
Homogenization distributes approved material lots throughout a defined batch, which reduces local differences in composition and feeding behavior. Incoming inspection, controlled blend ratios and final testing are still required: mixing cannot remove contamination, reverse polymer damage, or make incompatible materials compatible.
When I investigate unstable extrusion, I check the feedstock alongside the machine settings.
Recycled PP or HDPE may arrive from different collection streams, suppliers or production periods. The same polymer description on the bags does not make composition, melt behavior, color and contamination identical.
Research on batch fluctuations in post-consumer HDPE offers useful evidence: six consecutive batches, with material differences linked to changes in processing and product properties.
The practical lesson I take is that incoming variation has to be understood before deciding how to blend it.
| Variation to investigate | What controlled blending can do | What still needs separate control |
|---|---|---|
| Differences among approved resin lots | Distribute the selected lots more evenly | Incoming specifications and blend proportions |
| Uneven masterbatch distribution | Spread measured masterbatch throughout the batch | Dosing accuracy and melt-stage dispersion |
| Uneven filler or additive distribution | Improve the consistency of the premix | Powder handling, feeding, and compounding conditions |
| Moisture differences | Redistribute material without necessarily removing water | Drying and moisture testing |
| Foreign polymers, metal, or dirt | Potentially spread contamination through a larger batch | Sorting, inspection, separation, and filtration |
| Degraded or unsuitable resin | Blend it with other material without repairing it | Material acceptance and application testing |
I do not treat a large mixed batch as automatically better.
Blending one unsuitable lot into several acceptable lots can create a larger quantity of unsuitable material. So I approve the input lots and establish the recipe before loading the mixer.
I also avoid predicting a blended melt flow rate by simple arithmetic. Polymer melt behavior can depend on composition and interactions between materials, so the final blend is confirmed with the agreed test method.
My goal is repeatability: a controlled material supply that production can process inside a stable operating window.
I can weigh the right ingredients and still feed an uneven mixture. That gap changes material composition during an otherwise steady production run.
Premixing distributes measured ingredients before extrusion; post-pelletizing blending homogenizes suitable finished pellet lots. Both stay separate from melt compounding, where the extruder performs the melting, mixing and dispersion the final formulation needs.
I may place a mixer before the pelletizing line when approved recycled feedstocks have to be combined or a formulation prepared.
I may place it after pelletizing when cooled, suitable finished pellets have to be homogenized before packaging. Some plants need both stages.
| Mixing position | Purpose | Main checks |
|---|---|---|
| Before recycling extrusion | Blend approved recycled feedstocks | Polymer identity, contamination, moisture, and flow |
| Before compounding extrusion | Prepare a consistent recipe premix | Ingredient weights, distribution, and segregation |
| After pelletizing and cooling | Homogenize approved finished pellet lots | Pellet temperature, lot compatibility, and final quality |
| Before packing | Deliver a defined blended shipment | Sampling results, bag identification, and traceability |
Resin may be blended with color masterbatch, UV stabilizers, antioxidants, flame retardants or other additives.
I first check the physical form of each ingredient: a pelletized additive masterbatch presents a different mixing problem from a fine powder.
A suitable dry mixer distributes those ingredients through the batch. I do not claim that this step fully disperses pigments or breaks down every powder agglomerate.
For many compounds, the extruder’s screw design, temperature profile, residence time and feeding arrangement still develop the required melt quality.
I also consider whether an ingredient should enter through a separate feeder rather than a common premix. Reinforcing fibers, fine powders and low-dose additives do not all belong in the same loading sequence.
Coperion’s description of premix manufacturing is useful because it treats weighing, mixing, conveying and extruder feeding as connected steps.
My own selection follows that same process logic: the mixer is chosen together with the equipment that loads and unloads it.
I do not want to pay for unnecessary mixing complexity when the main task is homogenizing large quantities of suitable PP or HDPE pellets.
Our vertical screw silo mixers generally suit large batches of free-flowing plastic pellets and suitable clean, dry rigid flakes. I exclude powders and loose film from this standard design, and I do not recommend it for tacky elastomer or rubber materials.
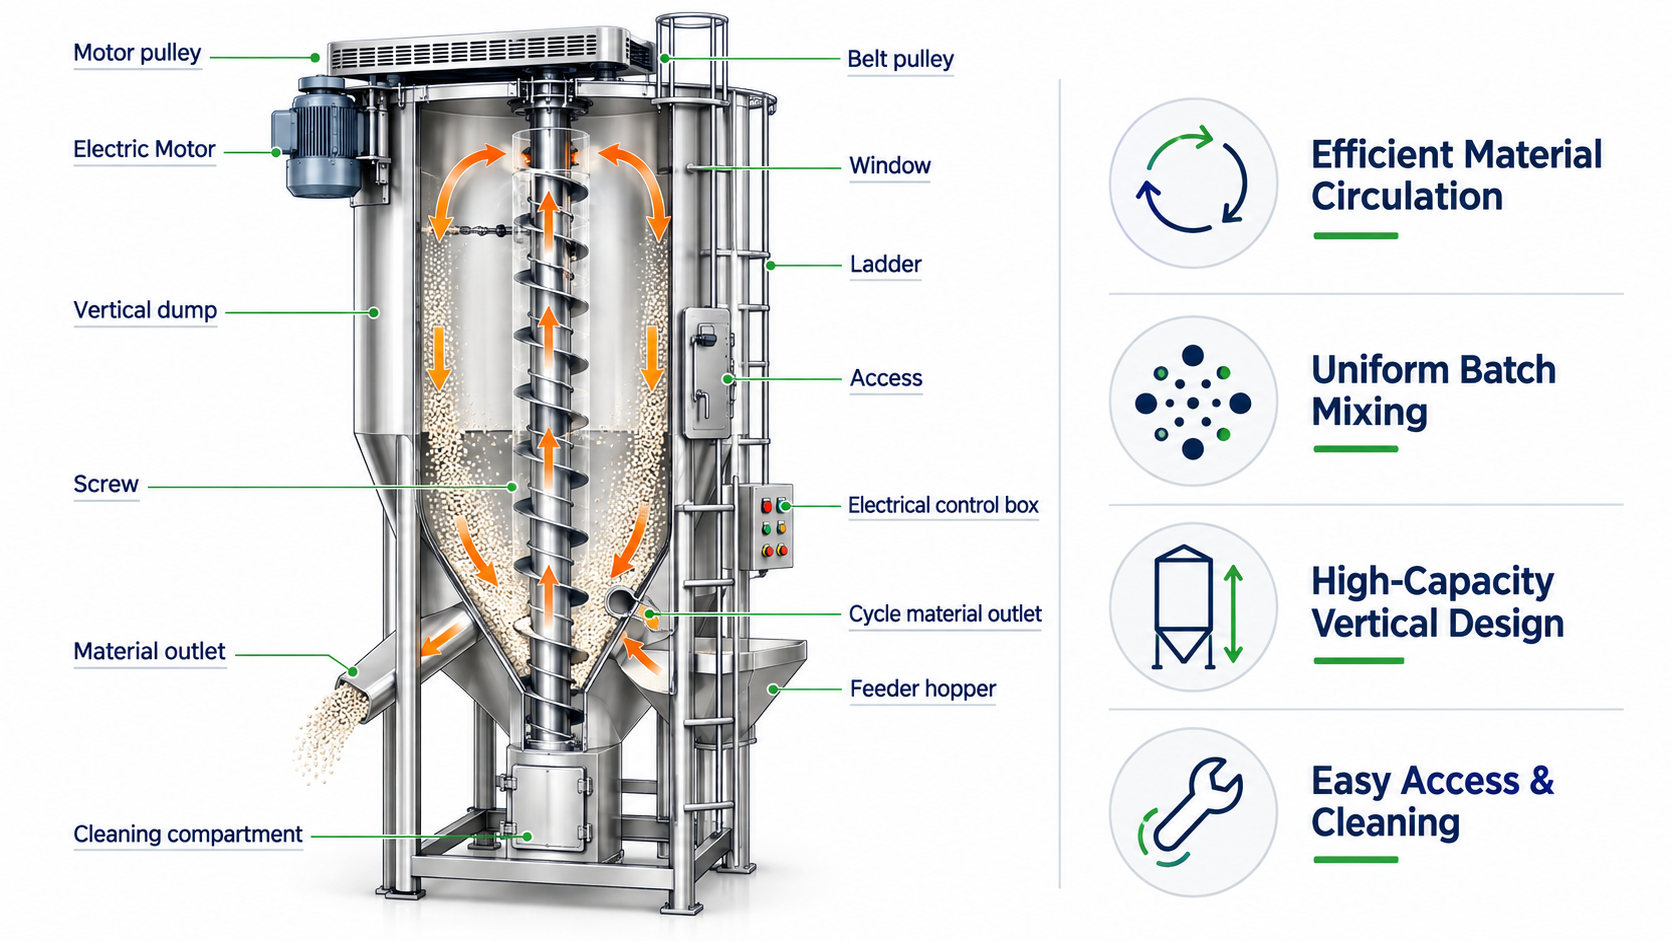
In this article I use “vertical silo mixer” to describe our vertical screw circulation design rather than every vertical mixing technology.
The screw lifts material through the central conveying section, and the material returns through the surrounding bulk, creating repeated circulation.
The process needs material that can move through the screw and return through the vessel reliably.
| Material or application | Usual position on Nicety’s standard vertical screw design |
|---|---|
| Free-flowing recycled PP pellets | A strong candidate for bulk homogenization |
| Free-flowing recycled HDPE pellets | A strong candidate for bulk homogenization |
| Suitable rigid PP or HDPE flakes | A candidate after checking size, dryness, and circulation |
| Other engineering plastic pellets | A candidate after reviewing heat sensitivity, abrasion, and moisture requirements |
| Fine powders or powder-rich formulations | A different mixing approach is selected |
| Loose plastic film | Not recommended for this design |
| Tacky elastomer or rubber particles | Not recommended for this design |
I do not recommend loose film because it can wrap around moving components, bridge, or circulate poorly.
Powder handling is also excluded from our standard vertical pellet-and-flake mixer. Powder applications need their own assessment of mixing action, sealing, dust control and discharge.
For elastomers and rubber, I pay close attention to friction and heat. Screw movement in the standard design can create local heating, and sensitive or tacky material may soften and adhere to the screw and nearby surfaces.
I regard that buildup as both a production problem and a cleaning problem. A lower purchase price offers little value when operators repeatedly stop the machine to remove sticky residue.
For suitable materials and approved shipping arrangements, our larger export vertical silo mixer configurations can reach approximately 15–20 metric tons per batch.
I treat that figure as a configuration range: actual working mass is confirmed against bulk density, usable volume, drive requirements and transport dimensions.
For large batches of ordinary free-flowing recycled HDPE or PP pellets, I usually find a vertical silo mixer more economical than a horizontal ribbon blender.
I still review building height, loading access, maintenance clearance and the strength of the installation area before recommending one.
I need a different mixing approach when powders, difficult additives or sensitive particles make a standard vertical screw mixer unsuitable.
Horizontal ribbon blenders suit suitable powder blends, pellet-and-powder premixes, and some free-flowing elastomer or rubber granules. I confirm material behavior through testing, and I do not treat a ribbon blender as a universal solution for sticky rubber masses, highly viscous compounds or every PVC formulation.
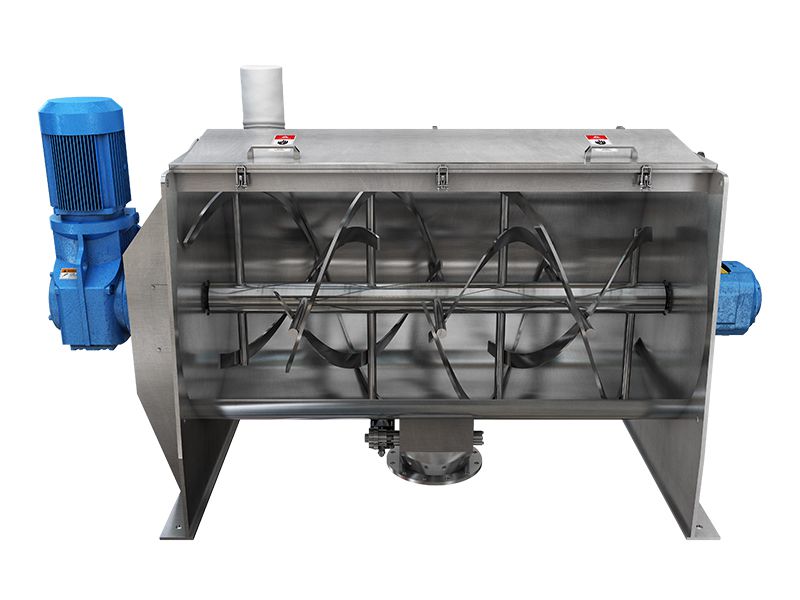
“Horizontal mixer” is a broad equipment description; a ribbon blender is one type of horizontal mixer.
In a typical ribbon blender, inner and outer helical ribbons move material in opposing directions along a horizontal trough, and that movement exchanges material across the batch.
I consider this arrangement when suitable resin powders, fillers, pigments and additives have to be blended before compounding.
I also review horizontal mixing for suitable elastomer and rubber granules, checking particle form, tackiness, temperature response and the torque needed to move the batch.
| Application | What to assess before recommending a ribbon blender |
|---|---|
| Resin powder with powdered additives | Flow, agglomerates, dust containment, and ingredient distribution |
| Pellets with powder additives | Density differences, powder adhesion, and later segregation |
| Free-flowing TPE or TPR granules | Heat generation, sticking, and discharge |
| Free-flowing rubber granules | Particle behavior, abrasion, and cleaning |
| Frequent color changes | Access to ribbons, seals, trough surfaces, and outlet |
| Sticky rubber masses | Whether a kneader or internal mixer is required |
| PVC formulations | Whether the process requires hot/cold high-speed mixing instead |
Speed and drive can be configured, but I still expect mechanical work to generate some heat.
Sensitive materials may need temperature monitoring or a cooling jacket, and I also assess whether a different agitator would suit a fragile or difficult product.
For rubber, I distinguish blending solid particles from working an uncured rubber mass. An ordinary ribbon blender is not offered as a replacement for a dedicated rubber compounding machine.
For PVC, I check the complete recipe and process. A required high-speed hot/cold mixing stage is not replaced with a ribbon blender simply because both machines handle powders.
For our usual container-shipped export configurations, the upper horizontal mixer capacity is generally approximately 5–6 metric tons per batch, subject to material density and final dimensions.
I present that as our practical export range, not a universal manufacturing limit for ribbon blenders.
Our horizontal machines generally cost more than comparable vertical silo mixing solutions, and the reason is worth stating: trough, agitator, drive, sealing and access requirements add cost.
I accept the higher cost when the material or the cleaning requirement makes the horizontal design the better production tool.
I can buy the cheaper mixer and still lose money through cleaning delays, poor discharge, or material that never reaches the required consistency.
The mixer is chosen by material form, flow behavior, heat sensitivity, recipe, batch volume and cleaning needs. I usually favor vertical silo mixing for bulk PP or HDPE pellet homogenization, and I consider horizontal ribbon blending when suitable powders, additives or sensitive granules need a different mixing action.
The following comparison covers our standard equipment configurations.
| Selection factor | Vertical silo mixer | Horizontal ribbon blender |
|---|---|---|
| Main application | Bulk homogenization of suitable pellets and rigid flakes | Suitable powder blends and more varied premixes |
| Common PP and HDPE pellet batches | Often the first choice | Possible, but the added cost has to be justified |
| Powder-rich recipes | Outside our standard design scope | A main application, subject to testing |
| Loose film | Not recommended | Assessed separately; suitability is not assumed |
| Tacky elastomer or rubber | Our standard screw design is not recommended | Trials required; another mixer type may be selected |
| Larger export batch range | Approximately 15–20 metric tons | Approximately 5–6 metric tons |
| Installation | Sufficient height and service access required | Sufficient floor area and service access required |
| Cleaning | Screw, vessel, and outlet access reviewed | Trough, ribbons, seals, and outlet access reviewed |
| Purchase cost | Generally lower for our bulk pellet applications | Generally higher in our comparable proposals |
I ask for bulk density rather than relying on the polymer name alone, and I calculate the required working volume as:
Required working volume = batch mass ÷ measured bulk density
For an illustrative 5,000 kg batch at a bulk density of 500 kg/m³, the figure is 10 m³ of material working volume; at 250 kg/m³ it is 20 m³.
I use those figures only to explain the calculation. They are not measured densities for a customer’s material.
I then account for the manufacturer’s permitted fill range and the space needed for effective material movement, keeping working volume distinct from total vessel volume.
ROSS’s ribbon blender specification guidance is a supporting reference for the relationship between batch volume, bulk density and equipment selection.
I include loading, mixing, discharge, inspection and cleaning when I estimate output.
For a line consuming 1,000 kg/h, a usable 5,000 kg batch represents five hours of feedstock — and preparing the next batch still needs time and buffer storage.
I would not describe a five-ton batch mixer as a five-ton-per-hour machine without establishing its full operating cycle.
I cannot prove uniformity by watching pellets move through an inspection window. Visible circulation does not show whether the full batch meets specification.
Mixing is confirmed through a written trial with representative material, defined operating conditions and samples from different discharge stages. Tests reflect the actual quality concern, and conveying and storage are checked afterwards to see whether the result survives to production.
I first identify the property that needs control.
For a colored formulation, I may compare color measurements on consistently prepared plaques. For a filler-containing formulation, ash testing may apply where the method suits the ingredients. For recycled pellets, melt behavior and other agreed properties may be assessed.
I do not use one test as proof of every aspect of uniformity.
| Trial detail to record | Why it matters |
|---|---|
| Input lot numbers and ingredient weights | To reproduce the batch |
| Material form and bulk density | To understand loading and circulation |
| Batch size and fill level | To confirm the intended operating range |
| Loading sequence, speed, and mixing time | To establish a repeatable operating procedure |
| Initial and final material temperature | To detect unwanted heating |
| Samples from early, middle, and late discharge | To check the material leaving the machine |
| Residue and cleaning time | To assess changeover and contamination risk |
I may create a satisfactory blend and then lose some of that uniformity during handling.
Differences in particle size, shape and density deserve particular attention, along with long drops, vibration, transfer lines and intermediate storage — all of which encourage ingredients to separate.
For a critical premix, I compare samples at the mixer discharge with samples near the extruder feed point, to establish whether the downstream system preserves the blend.
I also avoid assuming that longer mixing is always better. Extra time can add heat, wear or particle damage without improving the measured result.
At Nicety, recommendations rest on the material, the intended process and the results a trial can demonstrate. We do not promise a universal mixing time or a fixed quality improvement without supporting data.
I choose mixers to make material supply more consistent. The design is matched to the feedstock, the blend is validated, and handling is controlled through to production.
I identify the capacity ranges, material restrictions and relative pricing described here as company-specific guidance for Nicety equipment; final specifications are confirmed against the customer’s material and project requirements.
Sources
Only sources cleared to publish are listed; an article without a listed source is written from company practice.
Related
The equipment, solutions and projects the article relates to — chosen per article, not generated from keywords.
Equipment
Vertical screw batch mixer for large-capacity blending, batch homogenization, and color mixing of plastic pellets, regrind flakes, and granular masterbatches.

Equipment
Horizontal ribbon blender with counter-flow double helical ribbons for convective batch blending of polymer pellets, powders, regrind, and masterbatch without frictional heat build-up.
Application
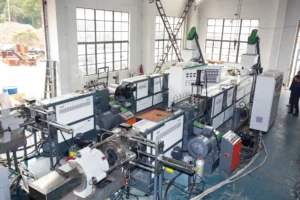
Rigid HDPE and PP scrap recycling line profile detailing shredding, vacuum extrusion, water-ring pelletizing, active VOC deodorization, and large-capacity vertical batch homogenization.
Case study
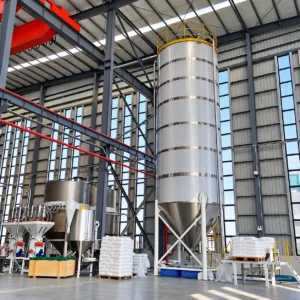
Industrial case study: 15-ton vertical pellet homogenization silo retrofit for an automotive PP compounding plant, reducing batch MFI variation from ±12.7% to ±1.1% (Cpk…
Case study
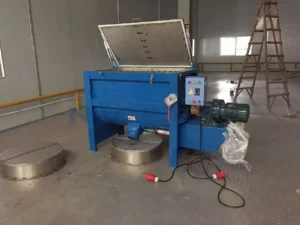
Industrial case study: sanitary 4,000L horizontal ribbon blender retrofit for a color masterbatch maker — dry cleanout cut from 95 to 18 minutes and…
Tell us the material, the process and what you need to achieve. Technical details can be completed later together with our sales team.