Auxiliary equipment & integrated systems
e-mail [email protected] Language EN ES PT

Application

Flexible & Cable Grade PVC Compounding and Extrusion Pelletizing Line

PVC extrusion pelletizing plant profile covering high-speed hot/cold compounding mixing, central vacuum transfer, and low-shear single-screw die-face pelletizing.

  • Plastic Extrusion Pelletizing Plants
  • Extrusion and Melt Processing
  • Feeding and Material Transfer
  • Mixing
  • Pelletizing
  • Post-Pellet Treatment
  • PVC
  • Pellets
  • Powder

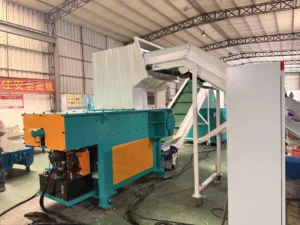
This industrial application profile outlines the dry blending, automated vacuum conveying, and single-screw pelletizing line architecture engineered specifically for PVC pelletizing plants producing flexible and semi-rigid polyvinyl chloride (PVC) pellets. Common applications include medical grade tubing, wire and cable jacketing, footwear soles, soft gasket extrusions, and automotive floor mats.

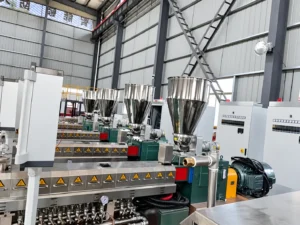
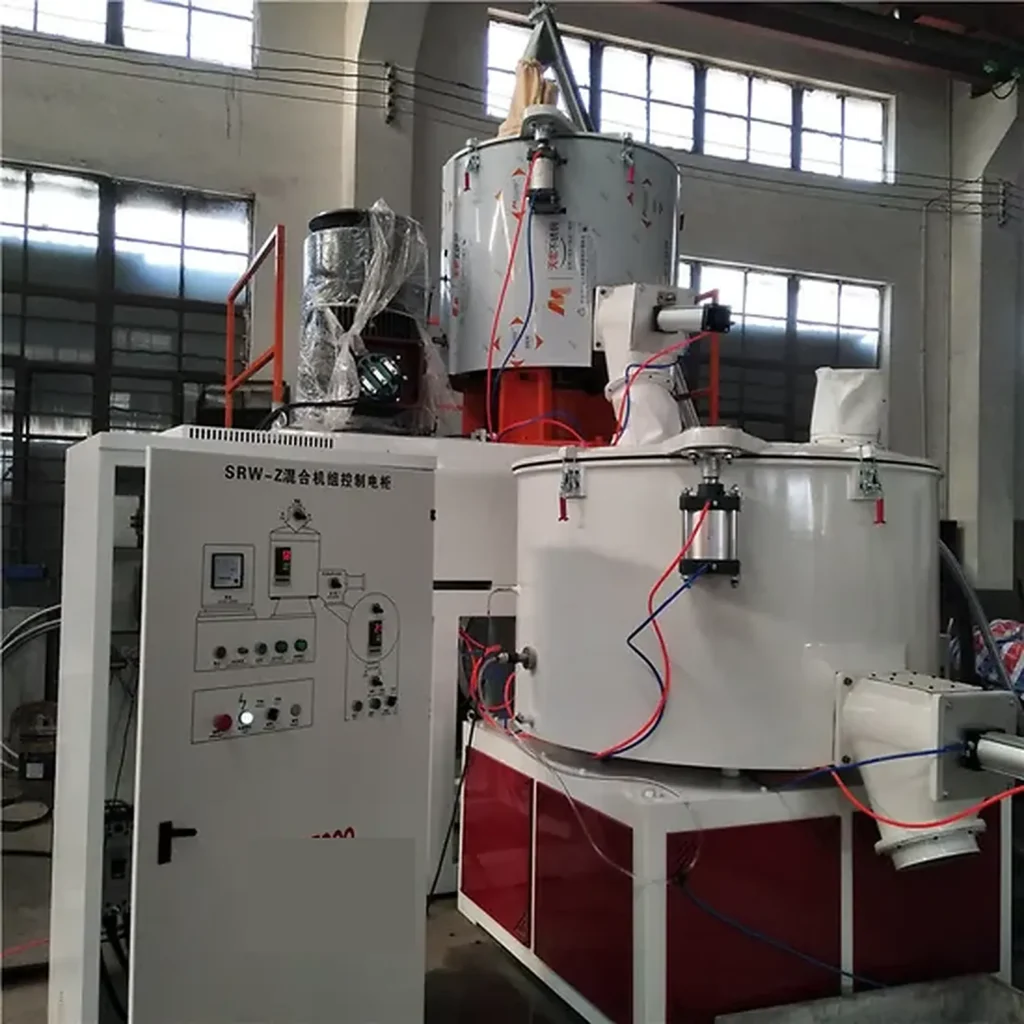
Processing plasticized PVC compounds requires precise thermal management and gentle shear control: high-shear compounding extruders overheat and degrade sensitive PVC polymers, triggering hazardous hydrochloric acid (HCl) gas liberation and burnt black discoloration. Conversely, insufficient pre-blending results in “sweating” pellets with unabsorbed liquid plasticizer puddles and inconsistent Shore hardness. This specialized application integrates a high-speed heating and cooling compounding mixer unit (SRL-Z series) for thorough plasticizer absorption (115°C–120°C hot mix to open PVC resin pores, followed by rapid cooling to 40°C), closed-loop vacuum conveying via a centralized feeding system, and a temperature-regulated low-shear single-screw extruder with die-face air/water-ring pelletizing, delivering bubble-free, perfectly plasticized, and crystal-clear PVC pellets.

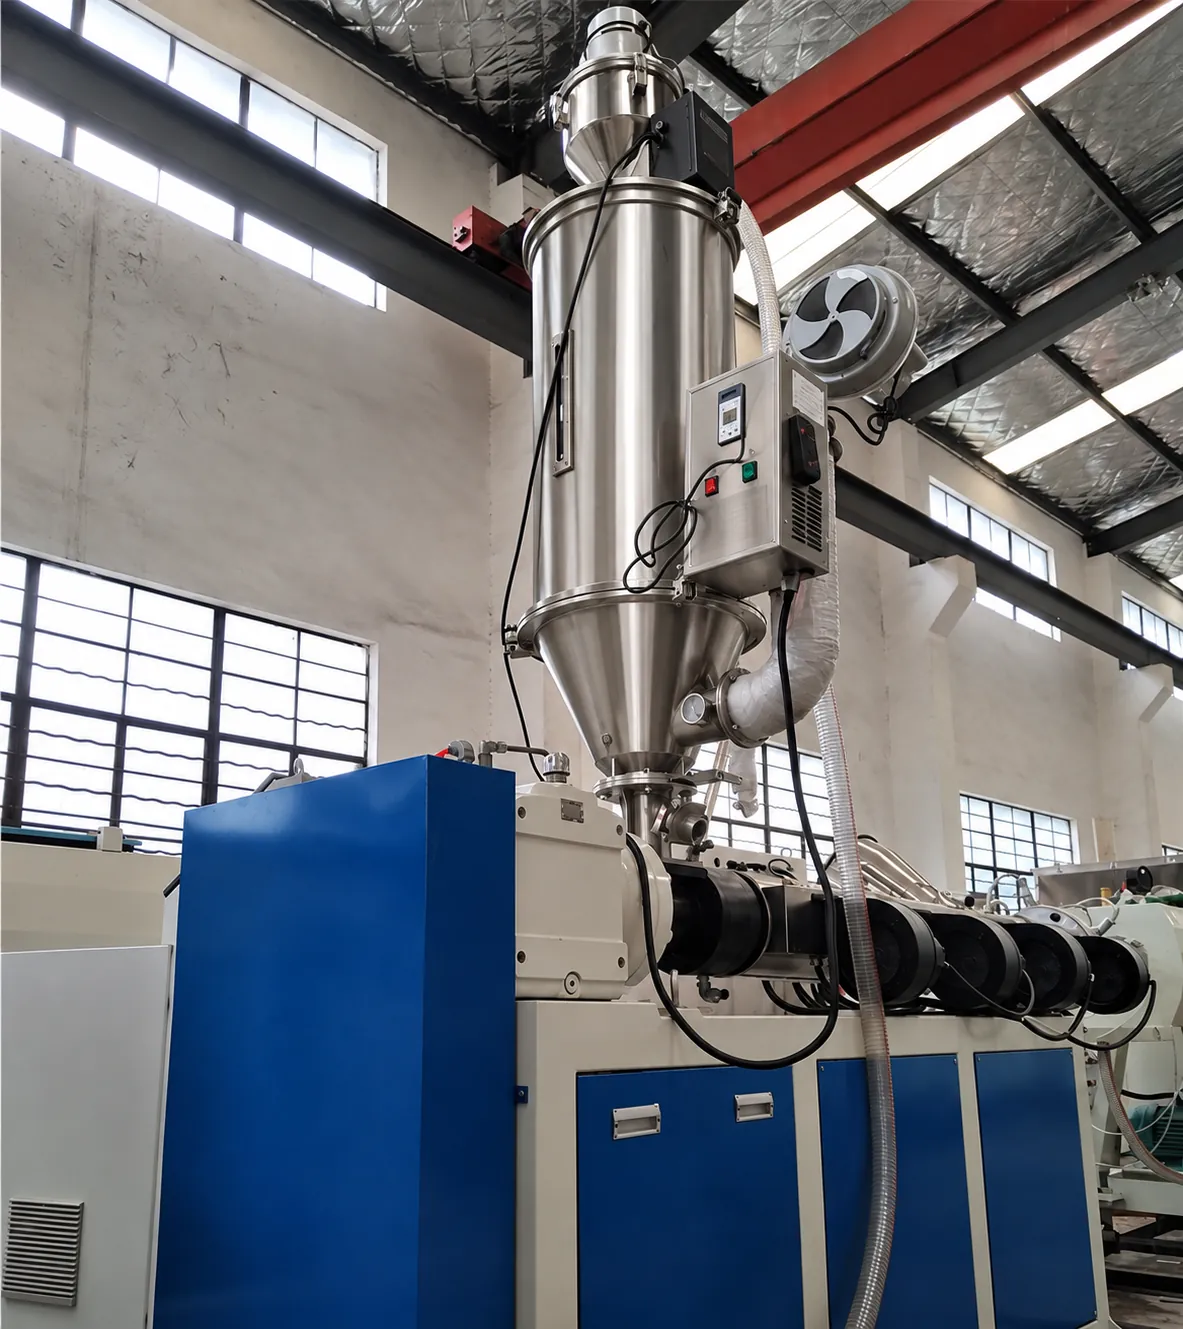
Photos

The scenario in practice

Photos of the scenario type, cleared to publish; the shots of a specific project live in its project record.

The scenario

Who runs it, what it makes, and what it must hold

Who it is for

PVC compounders, cable manufacturing plants, footwear compound suppliers, and extrusion pelletizing facilities producing soft and semi-rigid PVC granules.

Typical output

Clean, non-sticky flexible PVC pellets packaged in 25 kg multi-layer paper-plastic bags, ready for injection molding or extrusion of footwear, wire cables, medical tubes, and automotive trim.

Production goal

Produce dust-free, non-blooming, completely plasticized flexible PVC pellets with stable Shore hardness, zero black specks, and pristine surface clarity.

Process

The typical flow, step by step

The flow is the usual shape of the scenario; the machines for each step are chosen per project — see the solutions below.

  1. Bag Tipping & Powder Metering

    Feeding and Material Transfer

    Discharges PVC resin, mineral fillers, and additives into high-speed mixer charging port with dust collection.

  2. High-Speed Aerodynamic Hot-Mix Soaking

    Mixing

    High-speed aerodynamic impellers generate frictional heat up to 120°C, soaking liquid plasticizers deep into PVC grains.

  3. Jacketed High-Efficiency Cold-Mix Quenching

    Cooling

    Discharges hot dry-blend into lower cooling mixer, rapidly quenching material to 40°C via chilled water jackets to stop thermal history.

  4. Closed-Loop Central Vacuum Conveying

    Feeding and Material Transfer

    Transfers cooled dry-blend pneumatically through stainless vacuum pipes to the extruder feed hopper without powder segregation.

  5. Low-Shear Single-Screw Extrusion

    Extrusion and Melt Processing

    Plastifies PVC dry-blend under low shear and stable temperature, discharging molten polymer through a multi-hole circular die.

  6. Die-Face Hot Cutting & Spiral Elevator Cooling

    Pelletizing

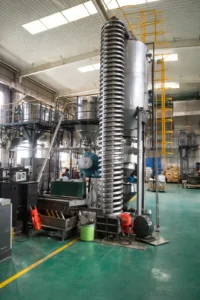
    Cuts polymer melt at the die plate, conveying pellets into a spiral cooling elevator for gentle final cooling and dedusting.

Where to go next

What Nicety builds for this scenario

Only our own solutions and machines are listed here. A complete line may also need equipment we don't make — that is specified per project.

Solutions for this scenario

Equipment and auxiliary machines

Equipment

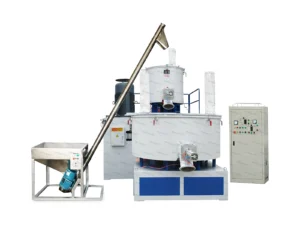
Compounding Mixer

High-speed compounding mixer (turbomixer / heating mixer) with high-shear aerodynamic fluidizing impeller for PVC dry-blending, masterbatch pre-mixing, and mineral filler coating.

Equipment

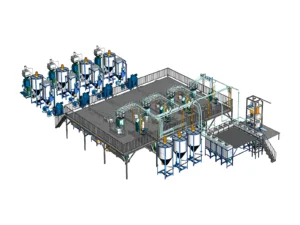
Central Feeding System

Plant-wide centralized pneumatic conveying and material distribution system for automated, closed-loop resin transfer to multi-station extrusion and molding lines.

Equipment

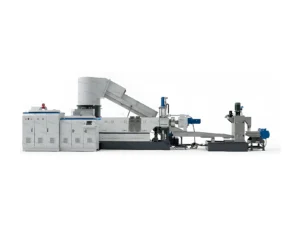
Single Screw Pelletizer

Heavy-duty single screw extrusion pelletizing system for cost-effective melting, vacuum degassing, and recycling of post-industrial rigid flakes and regrind.

Equipment

Water Ring Pelletizer

High-efficiency water ring hot-die face pelletizing system for cost-effective, strand-free pelletizing of PE, PP, masterbatches, and recycling regrind.

Equipment

Vibrating Spiral Elevator

Vertical vibrating spiral elevator for gentle upward conveying and intensive cooling of hot plastic pellets, available in Air-Cooled and Water-Cooled jacketed models.

Equipment

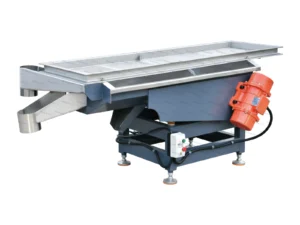
Linear Vibrating Screen

Industrial linear vibrating screen for plastic pelletizing lines, delivering continuous multi-fraction classification to scalp out agglomerates and eliminate fines and dust.

Material

What the line is fed

The properties named here are the ones the equipment questions turn on — they are confirmed per project, from samples where it matters.

Suspension PVC resin powder (K-value 65–70, bulk density 0.45–0.55 kg/L), liquid plasticizers (DOP, DOTP, DINP, DOA), Ca-Zn or organotin thermal stabilizers, stearic acid / PE wax lubricants, calcium carbonate fillers, and color pigments.

Requirements

What the process demands, and what quality is judged on

Critical process requirements

1. Controlled Frictional Heating & Plasticizer Soaking: High-speed mixer impellers convert kinetic energy into frictional heat, raising batch temperature to 115°C–120°C in 6–9 minutes to open porous PVC suspension resin grains, allowing complete plasticizer absorption.

2. Rapid Cold-Mix Quenching: Hot dry-blend drops automatically into the lower cooling mixer, cooling rapidly to ≤ 40°C in 4–6 minutes via chilled water jackets to stop thermal degradation and restore dry flowability.

3. Gentle Low-Shear Plastification: Single-screw extruder with deep-flighted feed zone and oil-cooled screw core gently plastifies PVC without localized shear overheating or thermal decomposition.

4. Die-Face Hot Cutting & Spiral Elevator Cooling: Molten PVC is sheared directly at the die head; pellets are pneumatically conveyed through a vibrating spiral cooling elevator to cool below glass transition before packaging.

Quality requirements

Plasticizer Absorption: Dry-blend powder must be 100% dry and free-flowing with zero liquid oil sweating on touch.

Thermal Stability: Congo Red test at 200°C ≥ 60 minutes, ensuring zero polymer degradation during extrusion.

Pellet Consistency: Uniform lenticular or spherical shape (Ø3.0 mm), Shore hardness variation within ±1 Shore A across full batch.

Selection

What decides the equipment in this scenario

These are the questions a quotation is built from — answering them up front shortens the first round.

SRL-Z heating and cooling mixer combination unit
Upper high-speed mixer (SUS304, 25–35 m/s tip speed) paired with oversized lower horizontal or vertical jacketed cooling mixer.
Closed-loop centralized vacuum feeding system
Airtight stainless piping and vacuum receivers to transfer fluffy dry-blend without environmental dust emissions.
Low-shear PVC single-screw extruder
Screw L/D 25:1 to 30:1 with internal oil cooling, barrel air blowers, and hard chrome-plated nitrided alloy flights.
Die-face air-cooling pelletizer or water-ring skid
Rotary die-face cutter with variable-speed motor and cyclone cooling receiver.

Fit

Where this scenario fits — and where it does not

The boundaries are part of the scenario: they keep equipment from being quoted into a case it cannot serve.

Best fit when

Best fit for PVC pelletizing plants manufacturing flexible PVC compounds (Shore 45A to 95A), PVC wire and cable insulation compounds, medical PVC pellets, and transparent footwear sole materials where complete liquid plasticizer absorption and gentle melt processing are mandatory.

Needs assessment when

Requires assessment when processing high-transparency crystal-clear medical PVC or food-contact grades, where liquid tin stabilizers, electropolished SUS316 contact surfaces, and dust-filtered cleanroom packaging enclosures are necessary.

Not suitable when

Not suitable for direct powder-to-pipe rigid PVC processing (where dry-blend powder is fed directly into conical counter-rotating twin-screw extruders without intermediate pelletizing).

Variants

How the scenario splits

A variant is written down only where the process and the decision actually differ.

Medical Transparent Flexible PVC

How it differs

Flexible PVC formulations with 40 to 80 phr DOP/DOTP plasticizer for transparent medical drip chambers and soft tubing.

Process difference

Requires liquid tin/non-toxic Ca-Zn stabilization, mirror-polished screw chrome-plating, and air-cooling die-face pelletizing to prevent water absorption.

Output difference

Crystal-clear, non-blooming pellets with light transmission > 90% and zero yellowing.

Flame-Retardant Wire & Cable Grade PVC

How it differs

Cable insulation and jacketing PVC formulations with 30 to 50 phr plasticizer, heavy CaCO3 filler (30–60 phr), and flame-retardant antimony trioxide.

Process difference

Requires heavy-duty hot/cold mixer with dual-tier high-shear impellers to fully disperse heavy mineral fillers and antimony synergists.

Output difference

Flame-retardant, high-dielectric-strength PVC pellets complying with UL94 V-0 and RoHS/REACH standards.

Before an inquiry

What we need to know to quote this scenario

  1. 01 PVC resin K-value and plasticizer loading (phr) Suspension PVC K-value (typically K-65 to K-70) and liquid plasticizer loading (phr = parts per hundred resin, 20 to 80 phr).
  2. 02 Stabilizer system and environmental constraints Calcium-Zinc (Ca-Zn), organic tin, or lead-based stabilizer system, plus regulatory compliance standards (RoHS, REACH, medical).
  3. 03 Target output capacity per hour Required pelletizing throughput (kg/h, typically 300 to 1,200 kg/h).
  4. 04 Cooling water utilities on site Available chilled water capacity (7°C–12°C, min 10–20 m³/h) for cooling mixer jacket and spiral elevator.

Request a Quote Send these points with your inquiry; the scenario can then be quoted against your line, not against an assumption.

Next step

Request a Quote

Tell us the material, the process and what you need to achieve. Technical details can be completed later together with our sales team.

Request a Quote
Request a Quote