Application
Automotive Bumper-Grade High-Impact PP Compounding Line (PP + POE / Talc)
Automotive exterior PP compounding profile covering twin-screw elastomer toughening, downstream talc side feeding, strand pelletizing, and vertical silo homogenization for bumper fascia grades.

This industrial application profile outlines the continuous high-speed compounding, dynamic impact toughening, and long-strand pelletizing engineering setup designed specifically for automotive polypropylene (PP) compounding plants. It focuses on producing high-crystallinity, high-impact modified polypropylene (PP + EPDM / POE elastomer + 10%–20% ultrafine talc) engineered for injection-molded automotive exterior bumpers, body side claddings, wheel arch liners, and instrument panel carriers.
Manufacturing automotive exterior PP compounds involves a classical engineering trade-off: achieving high cold-temperature impact toughness (-30°C to -40°C non-break Charpy) without sacrificing flexural modulus (stiffness > 1,800–2,200 MPa) and thermal dimensional stability. If virgin PP resin and POE elastomer are not subjected to sufficient dispersive and distributive shear, rubber domains agglomerate into large islands (> 2–5 µm), resulting in poor impact absorption, brittle failure, and ugly surface flow marks ("tiger stripes") during thin-wall bumper injection molding. Conversely, excessive shear overheating causes polypropylene chain scission, uncontrollable Melt Flow Index (MFI) spikes, and rubber phase thermal degradation. Furthermore, during post-extrusion strand pelletizing, high-viscosity elastomeric strands tend to stretch or deform in the cooling bath, causing inconsistent pellet cut lengths. This application integrates multi-component gravimetric feeding, a high-torque co-rotating twin-screw extruder with modular shear elements, downstream talc side-stuffing, continuous chilled-water bath cooling with high-velocity air-knife dewatering, heavy-duty tungsten carbide rotary strand cutting, and multi-ton vertical silo homogenization, delivering automotive-certified compound pellets with tight MFI control.
The scenario
Who runs it, what it makes, and what it must hold
Who it is for
Automotive plastics compounders, resin modification plants, and tier-1 polymer suppliers compounding impact-modified polypropylene for vehicle exterior and interior trim components.
Typical output
High-performance, dust-free cylindrical modified PP pellets packaged in 25 kg valve bags or 1,000 kg bulk big bags (FIBC), certified for direct tier-1 automotive injection molding of bumpers, exterior cladding, and instrument panels.
Production goal
Produce automotive OEM-certified high-impact PP compound pellets with sub-micron elastomer dispersion, zero tiger stripes in molded parts, low odor/VOC emissions, and lot-wide MFI variation ≤ 1.5%.
Material
What the line is fed
The properties named here are the ones the equipment questions turn on — they are confirmed per project, from samples where it matters.
Polypropylene base polymers: virgin PP impact copolymer or homopolymer pellets (bulk density 0.50–0.55 kg/L), metallocene polyolefin elastomers (POE / POP pellets, density 0.86–0.90 g/cm³), ultrafine surface-treated talc powder (D50: 1.5–3.5 µm), functional slip/anti-scratch additives, antioxidant packages (1010/168), and black masterbatch.

Process
The typical flow, step by step
The flow is the usual shape of the scenario; the machines for each step are chosen per project — see the solutions below.

-
Loss-in-Weight Gravimetric Feeding
Feeding and Material Transfer
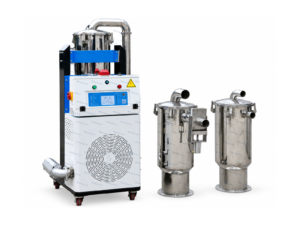
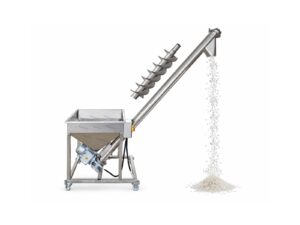
Transfers virgin PP pellets, POE elastomer granules, and additives gravimetrically into the main extruder feed throat.
-
Twin-Screw Compounding & Melt-Zone Talc Side-Feeding
Compounding
Melts PP and POE under high shear to achieve sub-micron rubber droplet morphology; twin-screw side feeder introduces talc into the melt pool.
-
Multi-Vent Vacuum Devolatilization
Extrusion and Melt Processing
Dual-vent high vacuum (-0.095 MPa) extracts trapped moisture, air, and volatile oligomers to guarantee low-odor automotive compliance.
-
Strand Water Bath Cooling & Dual Air-Knife Dewatering
Cooling
Extrudes continuous polymer strands into a temperature-controlled water bath to freeze polymer structure without strand elongation.
-
Tungsten Carbide Rotary Strand Cutting
Pelletizing
Precision tungsten carbide helical rotor shears parallel strands into exact cylindrical pellets with clean, vertical cut faces.
-
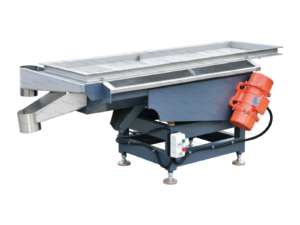
Linear Screen Classification & Dedusting
Post-Pellet Treatment
Dual-deck vibrating screen scalps off oversize doublets and dedusts micro-fines before transferring pellets to storage.
-
Large-Batch Vertical Silo Homogenization
Mixing
Circulates and folds 10 to 20 tons of finished pellets in a vertical silo mixer for 15 minutes, completely homogenizing minor process variations.
Requirements
What the process demands, and what quality is judged on
Critical process requirements
1. Sub-Micron Elastomer Dispersive Shearing: Specialized kneading screw zones impart high elongational and shear stresses to break down POE elastomer pellets into sub-micron droplets (0.3–0.8 µm) uniformly distributed within the PP matrix.
2. Downstream Talc Side-Feeding into Molten Core: Feeding ultrafine talc downstream via a twin-screw side stuffer prevents excessive screw flight wear and prevents powder aeration from choking the main feed throat.
3. High-Vacuum Devolatilization (-0.095 MPa): Dual-vent vacuum degassing removes moisture, peroxide byproducts, and volatile oligomers, ensuring compliance with automotive interior/exterior VOC standards.
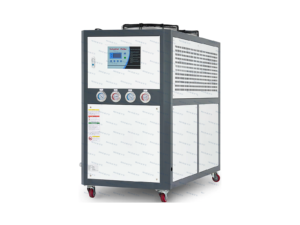
4. Controlled Strand Water Quenching & Vertical Silo Homogenization: Multi-pass stainless water bath with industrial water chiller maintains strand core crystallization temperature at 45°C–50°C for precision carbide cutting, followed by 15-ton vertical silo blending to eliminate lot-to-lot MFI drift.
Quality requirements
Low-Temperature Impact: Charpy notched impact at -30°C ≥ 35 kJ/m² (ISO 179) with 100% ductile failure.
Melt Flow Index (MFI) Consistency: MFI variation within ±1.0 g/10 min across the entire 10-ton production batch.
Pellet Morphology: Clean cylindrical cut (Ø2.5–3.0 mm x 3.0 mm length), zero agglomerates or long stringers, fines content (< 1.5 mm) strictly ≤ 0.05%.
Selection
What decides the equipment in this scenario
These are the questions a quotation is built from — answering them up front shortens the first round.
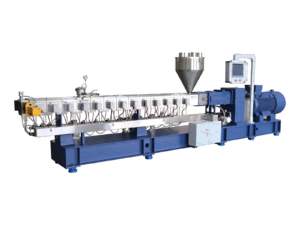
- High-torque twin-screw extruder with side stuffer
- Specific torque ≥ 10.5 Nm/cm³, L/D 44:1 to 48:1, bimetallic barrel liners, and vacuum de-aerated twin-screw side feeder.
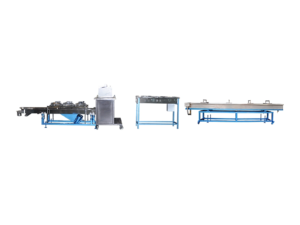
- Multi-pass temperature-controlled strand cooling bath
- SUS304 cooling trough with precision strand guide rollers, high-pressure air knives, and closed-loop temperature control.
- Heavy-duty tungsten carbide strand pelletizer
- Pneumatic feed roll pressure and cemented tungsten carbide helical cutter rotor for clean cylindrical cuts without dust.
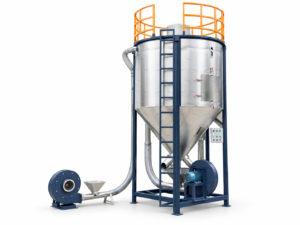
- Large-batch vertical homogenizing silo mixer
- 10 m³ to 20 m³ stainless steel vertical screw mixer to homogenize finished pellets and eliminate batch-to-batch MFI drift.
Fit
Where this scenario fits — and where it does not
The boundaries are part of the scenario: they keep equipment from being quoted into a case it cannot serve.
Best fit when
Best fit for automotive plastic compounding enterprises producing high-impact, high-flow modified polypropylene (PP) compounds toughened with 10%–25% POE (polyolefin elastomer) and reinforced with 10%–20% ultrafine talc powder for OEM exterior bumpers, rocker panels, body moldings, and interior pillar trims where stringent low-temperature impact and low tiger-striping are specified.
Needs assessment when
Requires assessment when processing ultra-high-flow thin-wall bumper grades (target MFI > 50–70 g/10 min) with high peroxide visbreaking levels, where specialized low-residence-time screw designs and high-speed water bath pullers must be calibrated to prevent strand sagging and strand breaks.
Not suitable when
Not suitable for direct long glass fiber roving pultrusion (PP-LGF) lines or crosslinked dynamic vulcanizates (PP/EPDM TPV) requiring curing agent reactive extrusion.
Variants
How the scenario splits
A variant is written down only where the process and the decision actually differ.
Automotive Bumper Thin-Wall PP Compound (High Impact)
- How it differs
High-melt-flow PP (MFI 25–45 g/10 min) compounded with 15%–20% POE elastomer and 15% ultrafine talc for thin-wall automotive bumper fascias.
- Process difference
Requires optimized shear screw profile to achieve sub-micron POE rubber domain morphology (D_avg ≤ 0.5 µm) and downstream side feeding of fine talc.
- Output difference
Charpy notched impact strength at -30°C ≥ 35 kJ/m² (non-break ductile failure), flexural modulus ≥ 1,900 MPa, and zero injection tiger stripes.
Low-Odor Automotive Interior PP Compound
- How it differs
PP impact copolymer compounded with 10% POE and 20% mineral filler for automotive door interior panels and instrument lower housings requiring low odor and low scratch resistance.
- Process difference
Requires deep multi-stage high-vacuum devolatilization (-0.095 MPa) with vacuum condenser to strip low-molecular-weight oligomers.
- Output difference
Low-VOC compound (odor level ≤ 3.0 according to VDA 270, total volatile organic compounds TVOC ≤ 50 µg/g) with scratch resistance Delta L* < 1.0.
Photos
The scenario in practice
Photos go here once real views of this scenario are cleared to publish.
-

Placeholder · 1200 × 900 px (4:3)(占位图) Replace with an approved application photo, real workshop or installation views at this size.(按此尺寸替换为正式图片。) -

Placeholder · 1200 × 900 px (4:3)(占位图) Replace with an approved application photo, real workshop or installation views at this size.(按此尺寸替换为正式图片。)
Before an inquiry
What we need to know to quote this scenario
- 01 PP resin grade and base MFI Virgin PP impact copolymer or homopolymer base resin MFI (typically 10 to 30 g/10 min).
- 02 Elastomer toughener specification POE type (octene or butene copolymer), density, and target loading percentage (10% to 25%).
- 03 Target mechanical and optical specs Required low-temperature Charpy impact (-30°C), flexural modulus, and automotive OEM VOC/odor test standard.
- 04 Target production capacity per hour Continuous compounding output (kg/h, typically 500 to 2,000 kg/h).
Request a Quote Send these points with your inquiry; the scenario can then be quoted against your line, not against an assumption.
Where to go next
The solutions and the equipment this scenario names
Solutions for this scenario
Solution
Continuous Strand Pelletizing, Inline Classification, and Automated Packaging Line
Integrated continuous st…
Equipment for this scenario